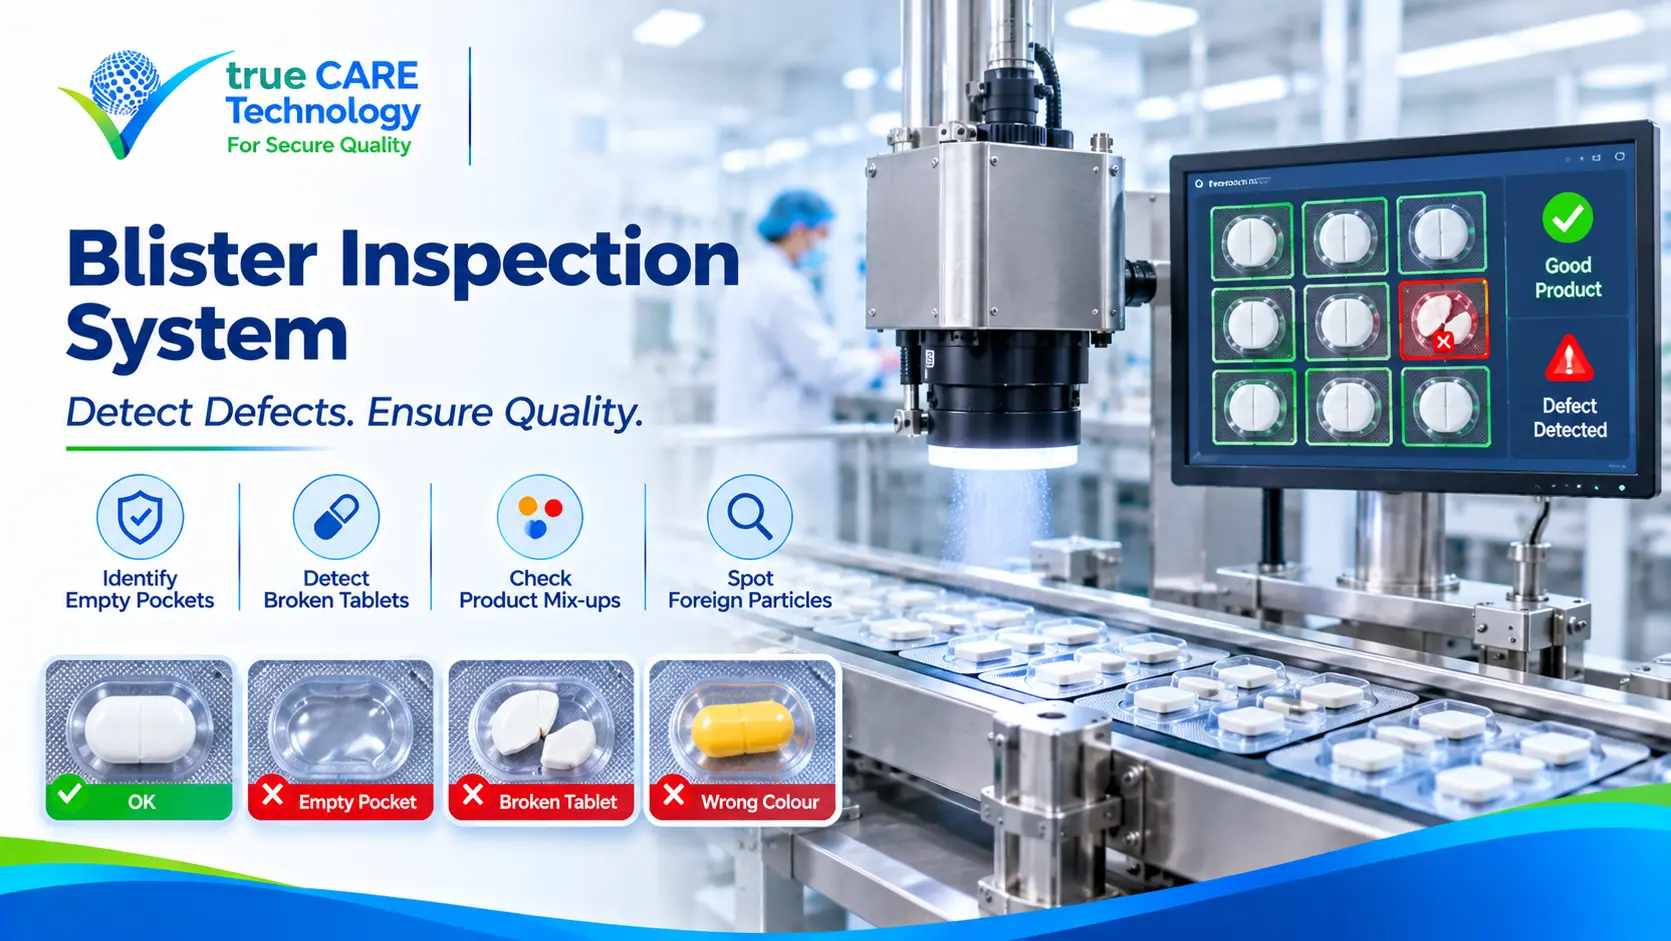
A blister strip with one empty pocket, a broken tablet or a tablet from the wrong product is a market complaint waiting to happen, and in the worst case a patient-safety event. A blister inspection system uses cameras and image processing to check every pocket on every strip at full machine speed, and rejects any strip that fails. This guide covers what these systems detect, where the camera goes, how each check works, and how to integrate and validate one.
Defects a blister system detects
TCT's Blister Inspection System is published to detect these defect types:
The system covers tablets (single or multi-colour, sandwich, coated, and white-on-white) and capsules (single or multi-colour, printed, gelatin, HPMC, pullulan, enteric-coated and granule-filled). Published minimum defect size is 0.3 mm, with inspection speeds of 1,000 blisters per minute and higher on some applications.
Camera placement
The camera is mounted on the blister machine after the pockets are filled and before the lidding foil is sealed. At that point every tablet or capsule is visible from above, sitting in its formed pocket.
Why before sealing?
Defects a blister system detects
TCT's Blister Inspection System is published to detect these defect types:
The system covers tablets (single or multi-colour, sandwich, coated, and white-on-white) and capsules (single or multi-colour, printed, gelatin, HPMC, pullulan, enteric-coated and granule-filled). Published minimum defect size is 0.3 mm, with inspection speeds of 1,000 blisters per minute and higher on some applications.
Camera placement
The camera is mounted on the blister machine after the pockets are filled and before the lidding foil is sealed. At that point every tablet or capsule is visible from above, sitting in its formed pocket.
Why before sealing?
- Visibility. Once aluminium lidding foil is applied, the top view is gone. Inspecting through the foil is not possible with standard cameras.
- Cheaper rejects. Rejecting before cutting and cartoning wastes less material.
- Root-cause feedback. Defects seen at the feeding stage point straight to the feeder.
Good placement also needs stable, even lighting. TCT uses a high-resolution industrial camera with specially developed illumination; one camera gives full top coverage, and more cameras can be added for wide formats or special products. Shield the camera from ambient light changes and vibration.
Colour, shape and size checks
Each check uses a different image property.
Presence and absence. The software compares each pocket region against the expected product. An empty pocket shows the forming film's colour and texture instead of a tablet.
Shape and size. The software measures the outline of each tablet or capsule: area, length, width and edge profile. Broken tablets show a smaller area and an irregular edge; chipped tablets show a notch in the outline; a double tablet shows a larger or overlapping shape. TCT publishes size-variation checks as a standard function.
Colour. The system compares each unit's colour against the taught reference. This flags wrong-colour product, coating defects, and mix-ups where a different product enters the feeder. Sandwich and multi-colour tablets are checked zone by zone.
Surface defects. Dark spots and foreign particles show as local contrast changes on the tablet surface.
White-on-white. White tablets in white PVC are the hardest case. Lighting angle and contrast settings matter. Ask your supplier to prove detection on your own white product.
TCT's software offers auto-teach and auto-tolerance setting, so a new product can be set up from good samples, and automatic correction when the forming foil changes.
Integration with the blister machine
The vision system works with the blister machine's own controls:
1. Trigger. An encoder or sensor tells the camera exactly when a strip is in position.
2. Inspect. Images are captured and analysed at line speed.
3. Track. The result is linked to that strip's position as it moves through sealing and cutting.
4. Reject. The vision system signals the blister machine to reject the failing strip at its reject station after cutting. TCT's system includes a high-speed I/O and ejection mechanism.
5. Confirm and stop. Consecutive-reject limits stop the machine so an operator can fix the feeder.
TCT's system includes a stainless cabinet, an industrial PC with touch screen and a threecolour tower lamp. The software is described as 21 CFR Part 11 compliant, with audit trail and production report generation. For Indian sites, revised Schedule M, enforced for all units since 1 January 2026, also expects validated computerised systems and data integrity.
Validation with challenge sets
A vision system is only trusted after you prove it catches every defect type it is meant to catch. That is done with challenge sets: known defective samples run through the system.
A typical challenge routine:
Colour, shape and size checks
Each check uses a different image property.
Presence and absence. The software compares each pocket region against the expected product. An empty pocket shows the forming film's colour and texture instead of a tablet.
Shape and size. The software measures the outline of each tablet or capsule: area, length, width and edge profile. Broken tablets show a smaller area and an irregular edge; chipped tablets show a notch in the outline; a double tablet shows a larger or overlapping shape. TCT publishes size-variation checks as a standard function.
Colour. The system compares each unit's colour against the taught reference. This flags wrong-colour product, coating defects, and mix-ups where a different product enters the feeder. Sandwich and multi-colour tablets are checked zone by zone.
Surface defects. Dark spots and foreign particles show as local contrast changes on the tablet surface.
White-on-white. White tablets in white PVC are the hardest case. Lighting angle and contrast settings matter. Ask your supplier to prove detection on your own white product.
TCT's software offers auto-teach and auto-tolerance setting, so a new product can be set up from good samples, and automatic correction when the forming foil changes.
Integration with the blister machine
The vision system works with the blister machine's own controls:
1. Trigger. An encoder or sensor tells the camera exactly when a strip is in position.
2. Inspect. Images are captured and analysed at line speed.
3. Track. The result is linked to that strip's position as it moves through sealing and cutting.
4. Reject. The vision system signals the blister machine to reject the failing strip at its reject station after cutting. TCT's system includes a high-speed I/O and ejection mechanism.
5. Confirm and stop. Consecutive-reject limits stop the machine so an operator can fix the feeder.
TCT's system includes a stainless cabinet, an industrial PC with touch screen and a threecolour tower lamp. The software is described as 21 CFR Part 11 compliant, with audit trail and production report generation. For Indian sites, revised Schedule M, enforced for all units since 1 January 2026, also expects validated computerised systems and data integrity.
Validation with challenge sets
A vision system is only trusted after you prove it catches every defect type it is meant to catch. That is done with challenge sets: known defective samples run through the system.
A typical challenge routine:
- Build the set. Prepare strips with one deliberate defect each: an empty pocket, a broken tablet, a chipped tablet, a wrong-colour tablet, an extra tablet and a foreign particle. Place defects in different pocket positions, including edges.
- Run at production speed. Feed the challenge strips into normal production at full speed.
- Record results. Every challenge strip must be rejected, and the reject must reach the reject bin.
- Test false rejects. Run good strips to measure how often good product is wrongly rejected.
- Repeat routinely. Run a reduced challenge at start-up, after changeovers and at set intervals during the shift.
TCT's system generates a challenge test report, which supports your IQ/OQ/PQ documentation.
See your strips inspected. Send TCT a few good strips and samples of your common defects. We will show you detection results and a challenge report. Request a free line assessment or product trial.
Frequently asked questions
Where is a blister inspection camera installed? After the pockets are filled and before the lidding foil is sealed.
Can it detect white tablets in white blisters? Yes, with suitable lighting and contrast settings, but always prove it on your own product.
How fast can TCT's blister inspection system run? It is published at 1,000 blisters per minute, with higher speeds possible on some applications.
See your strips inspected. Send TCT a few good strips and samples of your common defects. We will show you detection results and a challenge report. Request a free line assessment or product trial.
Frequently asked questions
Where is a blister inspection camera installed? After the pockets are filled and before the lidding foil is sealed.
Can it detect white tablets in white blisters? Yes, with suitable lighting and contrast settings, but always prove it on your own product.
How fast can TCT's blister inspection system run? It is published at 1,000 blisters per minute, with higher speeds possible on some applications.