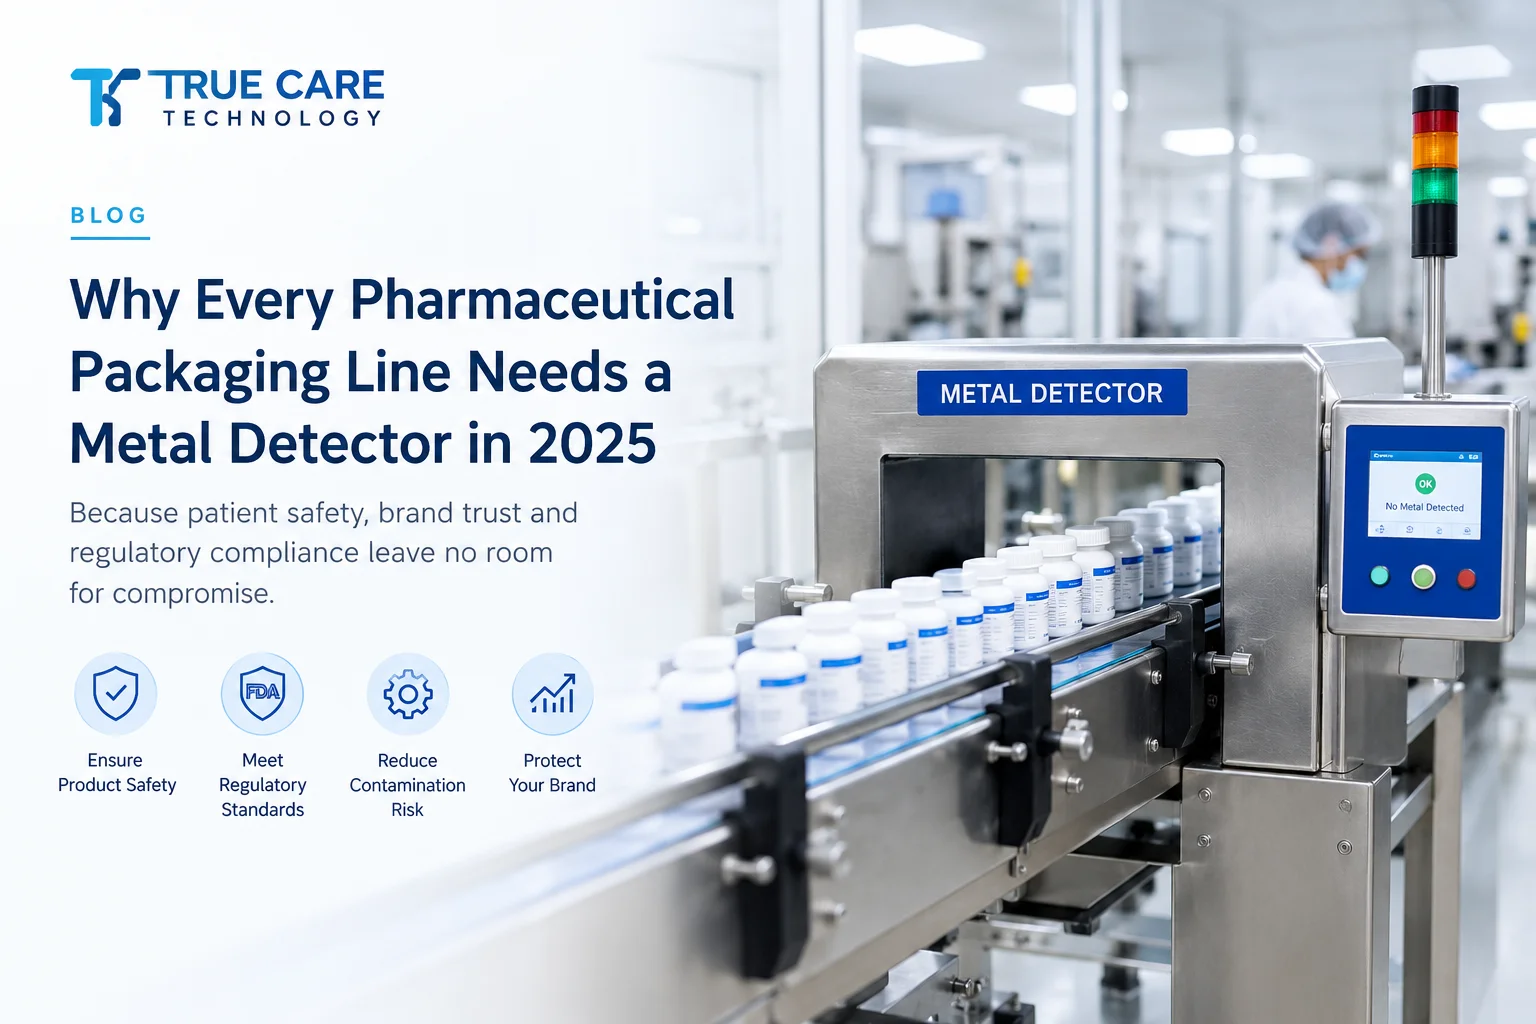
Regulatory expectations are rising, production lines are becoming more automated, and pharmaceutical manufacturers cannot afford to compromise on product integrity. Metal detection provides an important layer of protection against metallic contamination before products reach the market.
In pharmaceutical manufacturing, even a small metallic fragment can become a serious quality and safety concern. Metal particles can originate from equipment wear, broken machine components, damaged tooling, screws, needles, or other metallic parts used during production.
For manufacturers producing tablets, capsules, pills, powders, and other pharmaceutical products, integrating metal detection into the production or packaging process provides an additional control point for identifying and removing contaminated products.
Why Is Metal Detection Important in Pharmaceutical Manufacturing?
Pharmaceutical production involves numerous high-speed mechanical processes. Tablet presses, capsule filling machines, conveyors, feeders, packaging equipment, and other machinery operate continuously and can introduce the possibility of foreign-metal contamination.
A metal detector helps identify contaminants such as:
- Ferrous metals such as iron and steel
- Non-ferrous metals such as copper and aluminium
- Stainless steel
- Small metallic fragments generated through equipment wear or mechanical damage
By detecting contamination automatically, manufacturers can prevent affected products from continuing through the production and packaging process.
True Care Technology's pharmaceutical metal detectors are designed specifically for tablets and capsules and can be integrated after processes such as tablet compression and capsule filling.
Five Reasons to Integrate a Metal Detector Into Your Pharmaceutical Line
1. Protect Product Quality and Patient Safety
Product quality is one of the most important considerations in pharmaceutical manufacturing.
Metal contamination may not always be visible during conventional visual inspection. An automated metal detector provides an additional inspection stage capable of identifying metallic contaminants that could otherwise pass through the production process.
Metal contamination may not always be visible during conventional visual inspection. An automated metal detector provides an additional inspection stage capable of identifying metallic contaminants that could otherwise pass through the production process.
The contaminated product can then be automatically rejected, reducing the possibility of defective units reaching subsequent packaging stages or the market.
2. Detect Multiple Types of Metal Contamination
Modern pharmaceutical metal detectors are designed to detect more than just iron.
Depending on the system and application, detection can include:
Ferrous metals → Non-ferrous metals → Stainless steel
This is particularly important because stainless steel is commonly used in pharmaceutical manufacturing environments, while aluminium, copper, and other metals may also be present in machinery or processing equipment.
True Care Technology's Pharma Metal Detector is designed to detect ferrous, non-ferrous and stainless-steel contaminants in pharmaceutical products.
3. Reduce the Risk of Contaminated Products Moving Forward
A metal detector is most effective when it is integrated into the production flow at an appropriate inspection point.
When contamination is detected, the system can trigger an integrated rejection mechanism so that the affected product is removed from the production stream.
This creates a simple process:
Production → Inspection → Detection → Automatic Rejection → Verified Product
Automated rejection also helps reduce dependence on manual inspection and supports continuous production.
True Care Technology systems include rapid integrated rejection mechanisms intended to minimize product waste while maintaining inspection efficiency.
4. Support Consistent Quality Control
Manual inspection alone can be difficult to maintain consistently on high-speed pharmaceutical production lines.
Automated detection provides a repeatable inspection process that can operate continuously with defined sensitivity settings.
TCT's pharmaceutical metal detection systems incorporate digital signal processing, touchscreen operation, product settings and data-storage capabilities to support controlled operation across different applications.
5. Integrate Inspection Into Existing Production Lines
A metal detector does not necessarily need to operate as a standalone machine.
Depending on the application, inspection can be integrated with equipment used for tablets, capsules, bottles, powders, or other pharmaceutical products.
For example, tablet and capsule metal detectors can be positioned after compression or encapsulation and before subsequent packaging stages.
For bottle-based applications, conveyorized metal detection can inspect products moving through an automated conveyor system.